What is Closed-Loop Manufacturing ?
TALK WITH OUR EXPERTSClosed-loop manufacturing is a way of controlling a production process in which part measurements are automatically turned into machine corrections. The part is measured, the right adjustments are calculated, and they are applied to the machine, closing the loop between measurement and production.
It builds on SPC (Statistical Process Control) but goes one step further: instead of only detecting when a process drifts, it calculates and applies the correction. Clooma’s approach was developed from the research of Professor Maurice Pillet and the SYMME laboratory at the University of Savoie Mont Blanc in France.
In machining, closed-loop manufacturing rests on two principles:
- Controlling complex processes, by managing the simultaneous correction of dozens of tool offsets
- Correcting process drift, through damping functions that react to real drift, not to normal variation
Closed-loop manufacturing: three meanings, one focus
The term « closed-loop manufacturing » is used in several contexts:
- Circular economy: reusing scrap and end-of-life products as raw material.
- Product lifecycle management: feeding production and field data back into product design.
- Process control: feeding part measurements back into machine settings during production.
This article focuses on the third meaning, as applied to precision machining, where closed-loop control directly reduces scrap and setup time.
How closed-loop manufacturing works in machining?
In a machine shop, closed-loop manufacturing runs as a simple cycle:
- Measure. The operator measures one or several parts with the shop’s measuring equipment.
- Calculate. The software analyzes the results against the tolerances and the process history, and calculates the adjustments needed.
- Correct. The tool offsets are sent back to the CNC, with no manual calculation or entry.
The operator no longer has to work out which offsets to change, or by how much. The software does it, consistently, on every shift.
Principle 1: controlling complex processes
Why manual adjustment is so difficult?
On complex parts, dimensions are interdependent: changing one tool offset affects several characteristics at once. Setting up the machine quickly becomes a puzzle.
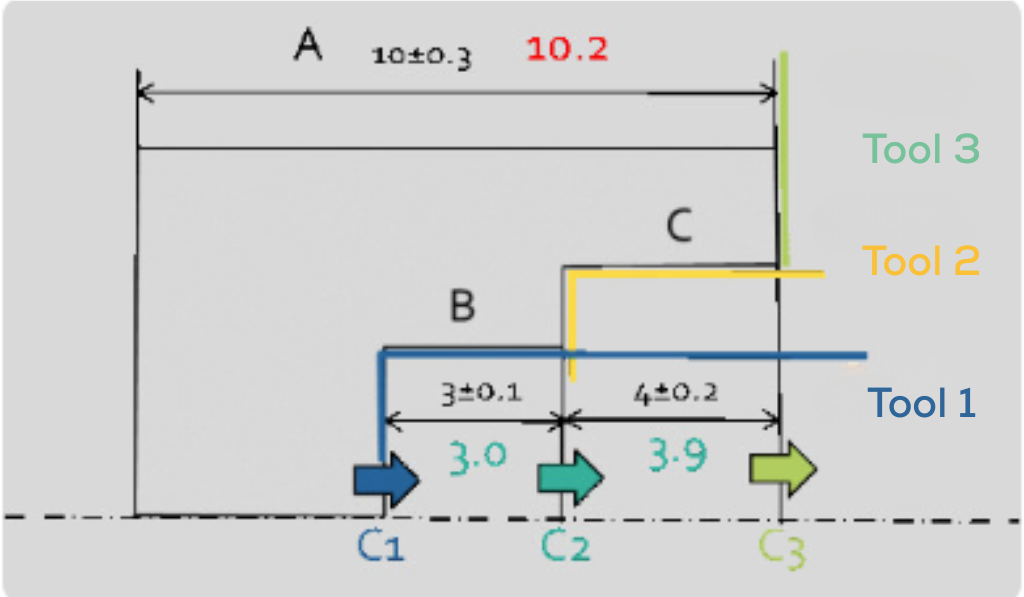
Take the example above. Dimension A measures 10.2 and is out of tolerance. To correct it, you need to adjust tool T3. But T3 also affects dimension C, which is currently within tolerance. So you must also adjust tool T2, which in turn affects dimension B, and so on.
The operator now has to figure out how to adjust T1, T2 and T3 together to bring A back into specification without pushing B or C out.
This example is simple. Real parts often have dozens of characteristics and tools, and working out the right combination by hand can take a significant amount of time, with a high risk of error.
How Clooma calculates the optimal adjustment?
Closed-loop manufacturing software such as Clooma calculates the optimal adjustment for every tool automatically. It relies on a configuration that can be built in two ways:
- from the individual impact of each tool, or
- from a 3D measurement file of the part.
From the individual impact of each tool
Configuring Clooma means defining how each tool offset affects the measured characteristics. The question to ask is simple: if I change this offset, which dimensions will move?
This is done only once, when the part is industrialized. From then on, Clooma’s algorithms calculate the required adjustment for each tool automatically. For example:
T1: -0.3 mm · T2: -0.3 mm · T3: -0.2 mm
From a 3D measurement file
Configuration is even simpler with a 3D measurement file. You import the file and specify which types of correction the machine uses. Clooma’s algorithms handle the rest and compute the optimal settings.
Whichever method you choose, the result is the same: the operator no longer performs any manual calculation. The right adjustments are provided automatically.
Principle 2 : Correcting Process Drift
The limits of SPC (Statistical Process Control)
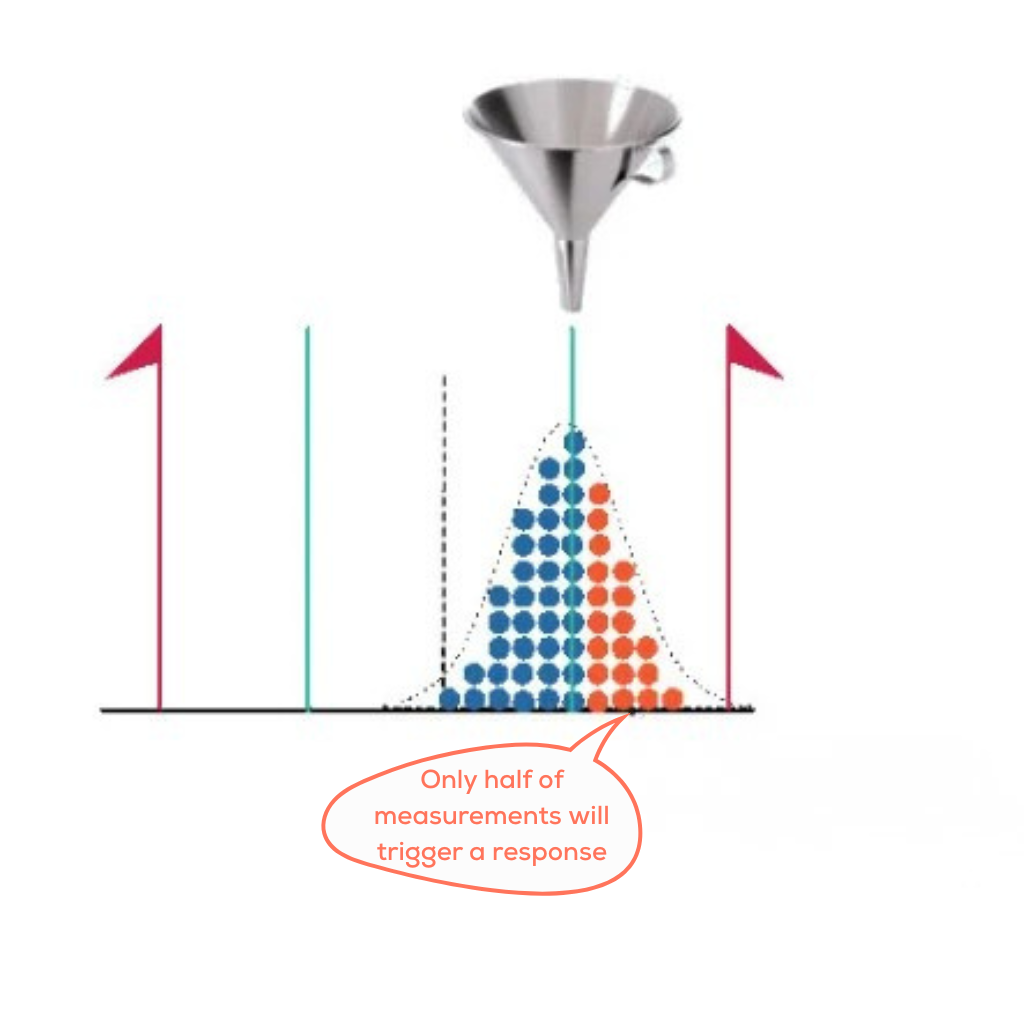
With SPC, control charts are used to monitor variation. The process is considered stable as long as measurements stay within the control limits. When a point falls outside them, the process has drifted and must be adjusted.
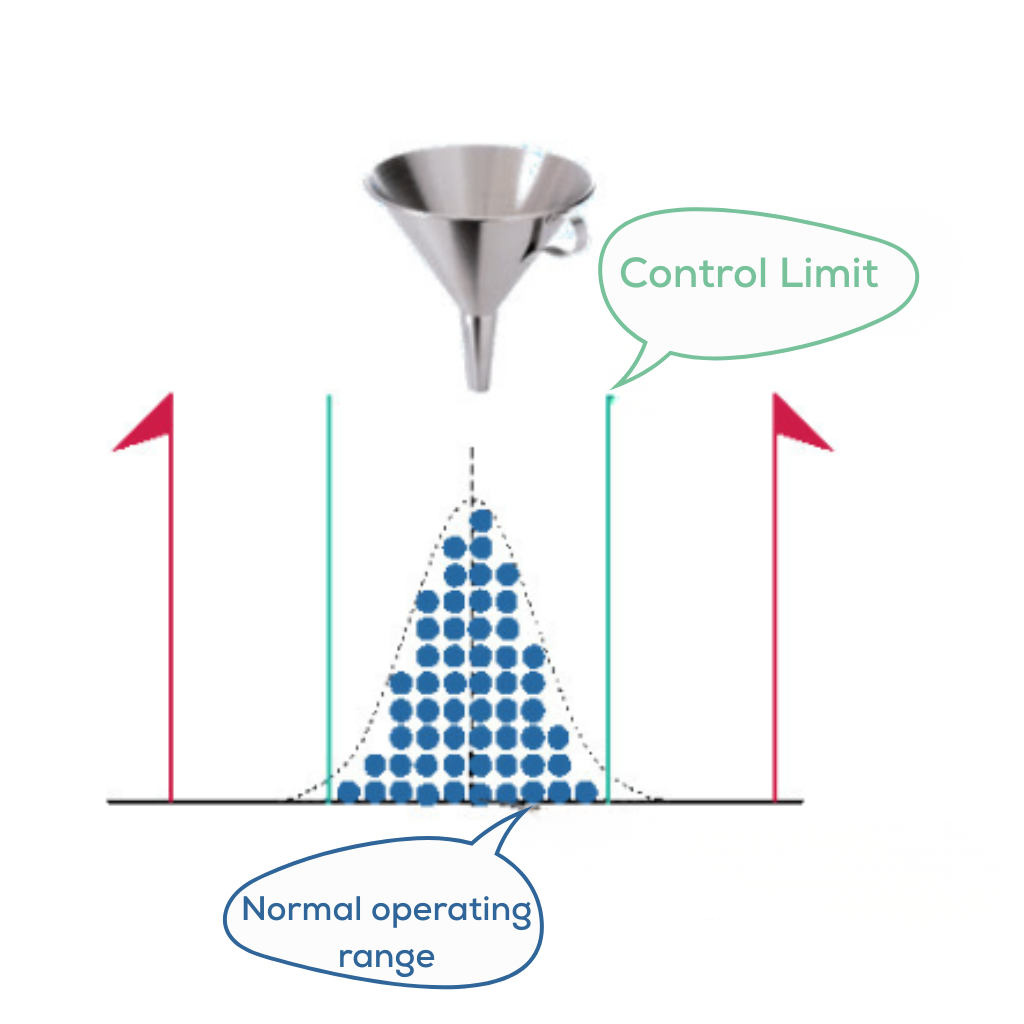
The problem is that SPC only reacts once the process has already drifted significantly. In the example below, the process has clearly started to drift, yet only about half of the measurements fall outside the limits. By the time corrective action is triggered, it is already late.
How damping functions correct drift
SPC works on a binary logic: inside or outside the limits. Calculating adjustments digitally makes much finer control possible.
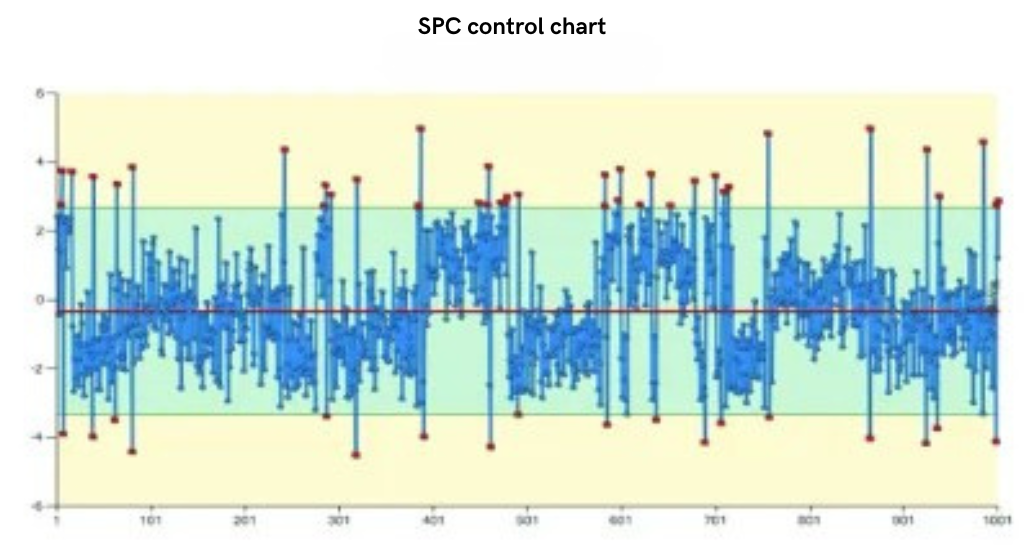
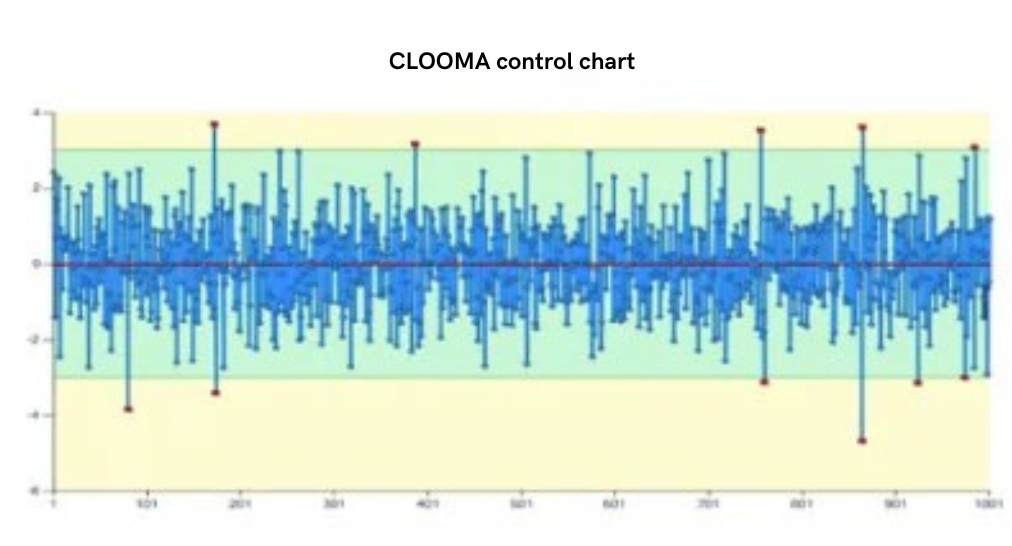
With Clooma, the process is assessed at every measurement. The software calculates a correction proportional to the drift, weighting each new result against the process history. Small random variations are damped out rather than chased, while real drift is corrected well before it reaches the tolerance limits.
The two charts below show the same process, first monitored with traditional SPC, then corrected with Clooma.
Process monitored with traditional SPC :
Same process monitored with CLOOMA software :
Benefits of closed-loop manufacturing
Compared with traditional process control, closed-loop manufacturing:
- Reduces setup to a single part. With automated adjustment, one part is enough to set up the machine. For example, a gearbox housing that used to take half a day to set up can now be adjusted in about 30 minutes, a single production cycle.
- Cuts scrap. Fewer setup parts and fewer out-of-tolerance parts in production. LISI, for example, reduced its scrap rate by 95%.
- Improves process capability. Ppk values above 1.33 on critical characteristics become achievable.
- Handles complexity. Dozens, even hundreds, of characteristics are monitored at once, and the relationships between offsets are calculated automatically.
- Removes human error. No more calculation or sign errors, and the same adjustment logic across every shift and team.
- Is quick to adopt. Operators can be trained in a single day.
Conclusion
By automating process adjustment, closed-loop manufacturing reaches quality levels that manual methods and traditional SPC cannot, while freeing machine time lost to setups and corrections.
Clooma was built from the ground up on these principles. Whether you need to control a complex part or keep a drifting process in tolerance, it takes the calculations off the operator and brings a new way of running process control to your shop floor.
Have more questions?
Read our FAQ or see the LISI case study.
Let's talk about your factory